



-
1–3 days expedited prototype manufacturing & flexible, responsive supply chain fulfillment
-
Firm commitment to on-time shipment and consistent premium product quality
-
Comprehensive material options + full range of industrial standard surface finishing treatments
-
Factory-direct quotation & fully open, transparent cost breakdown
-
Quality system certified to ISO 9001:2015 / IATF 16949:2016 standards
-
Turnkey integrated assembly service: We supply complete finished usable goods and standalone spare parts
One-stop Custom Metal Service From Prototyping to Mass Production
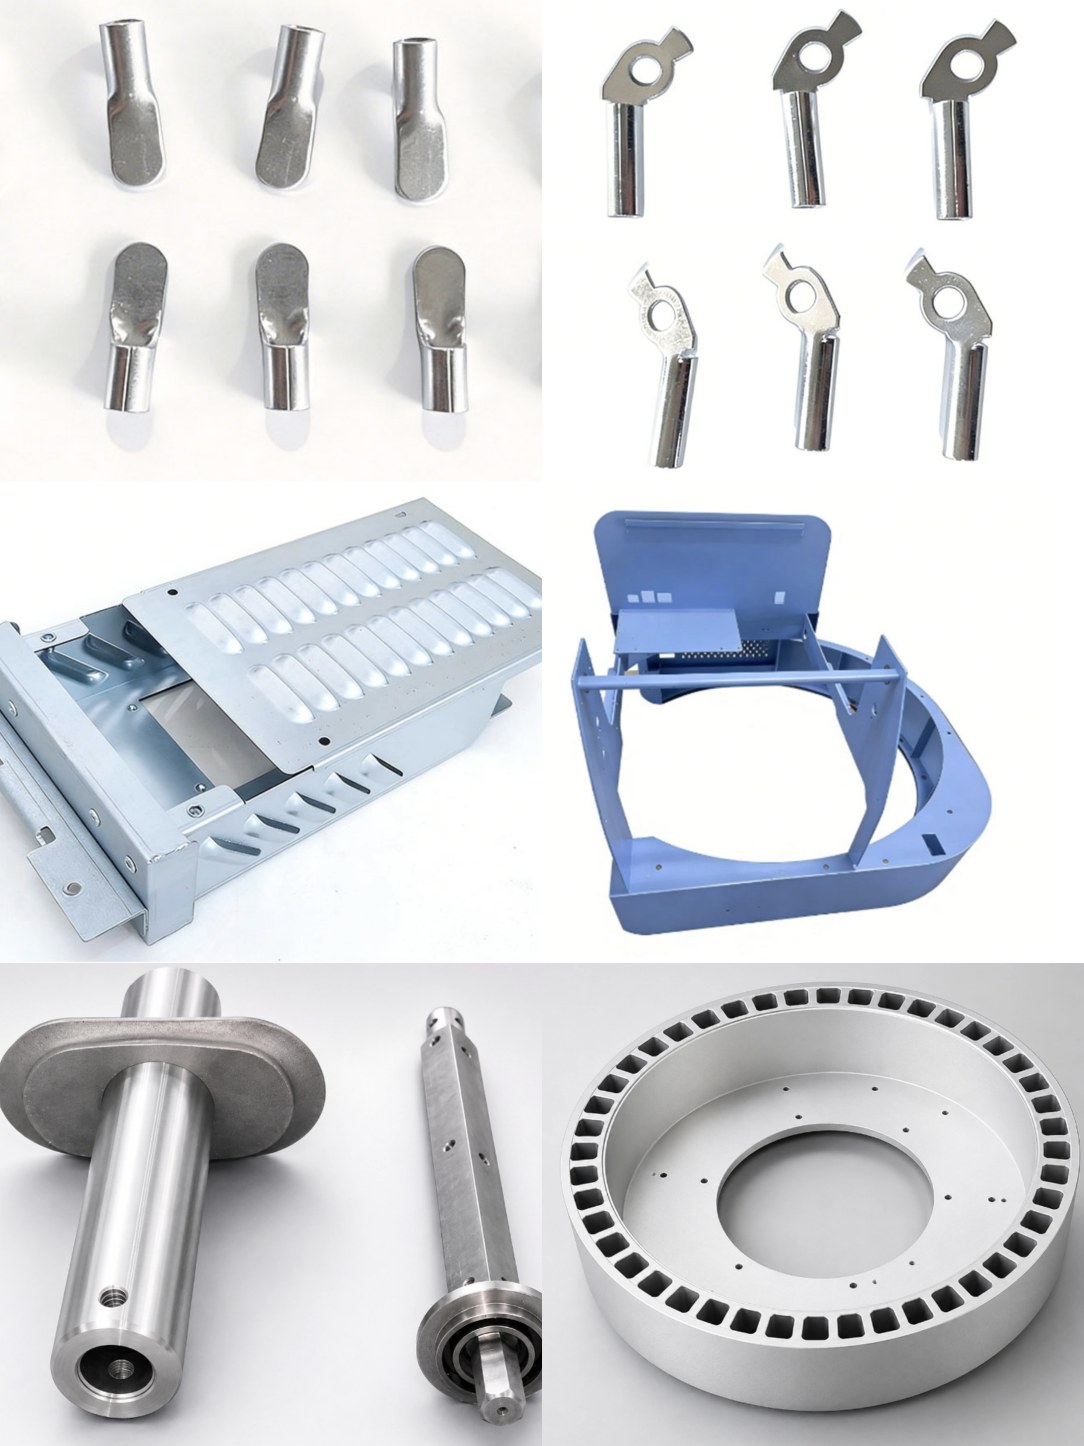
support diverse engineering and manufacturing applications.
-
Competitive Prices & DFM
-
24/7 Engineering Support
-
Quick Turn, Short Lead Time, not MOQ
Verify Certifications On Demand: IS0 9001:2015|IATF 16949:2016
about chuangkai
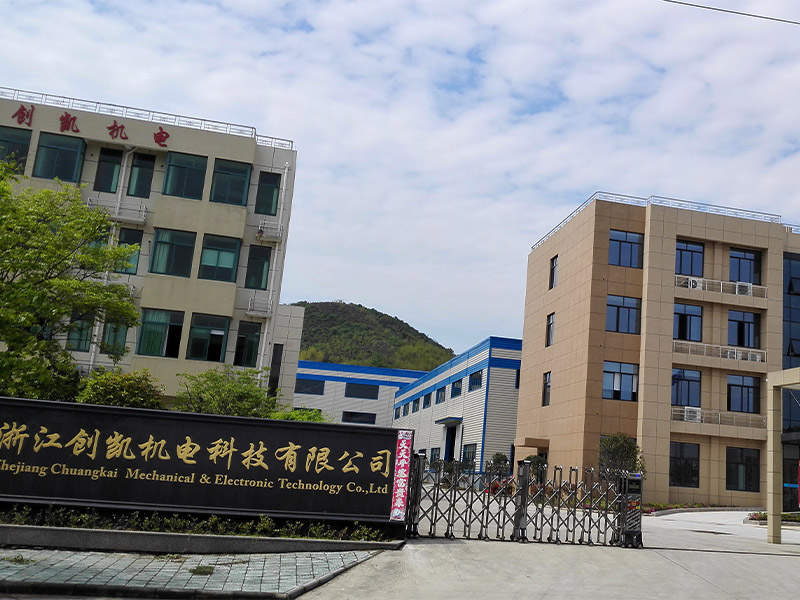
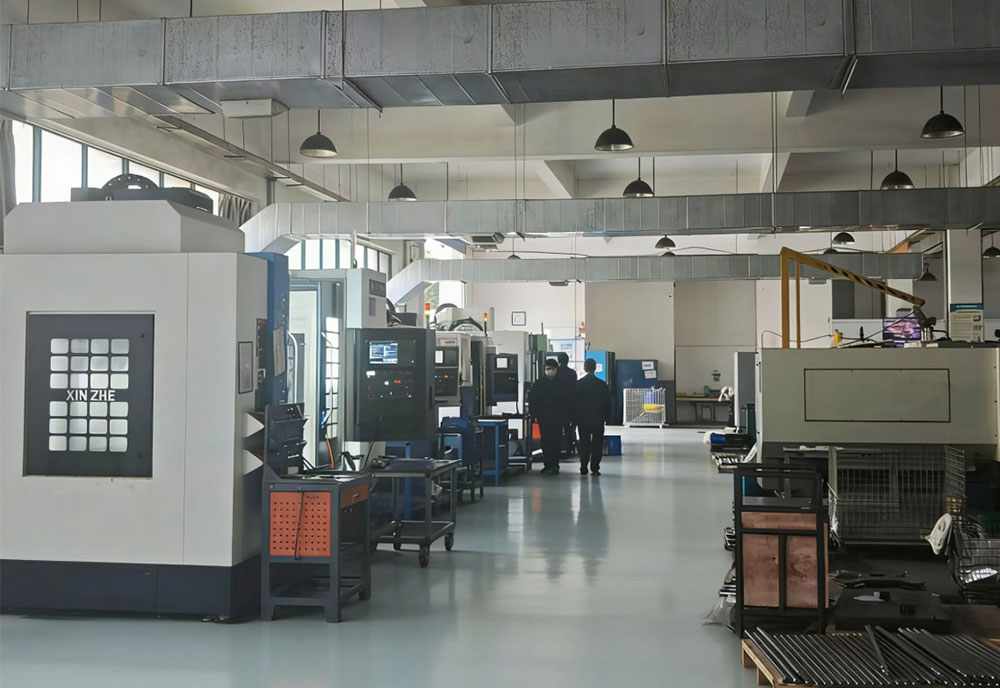
Zhejiang Chuangkai Mechanical and Electrical Technology Co., Ltd. was established in March 2003, with a registered capital of 15 million RMB. The company is a high-tech enterprise integrating the design and manufacturing of precision tooling, precision metal stamping, precision sheet metal processing, precision machining, surface painting, powder coating, and assembly of precision components.Currently, it has 95 employees and possesses advanced precision processing equipment and standardized workshops, with a total area of approximately 13,500 square meters. We have obtained ISO9001, IATF16949,ISO45001, ISO14001 system certifications.
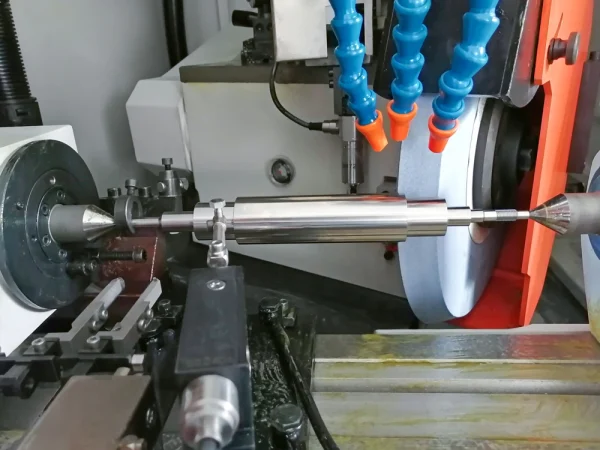

Precision stamping tooling design & manufacture
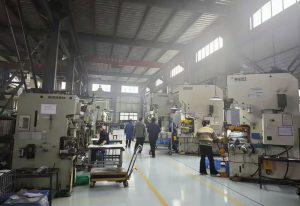
Main stamping equipment in the stamping workshop: 18 sets of high-speed precision punch presses with specifications such as 16 tons, 25 tons, 40 tons, 60 tons, 80 tons, 110 tons, 200 tons and 250 tons. The speed of the precision high-speed punch press can reach 500 times per minute.
Materials for stamping processing: brass, phosphor bronze, beryllium bronze, nickel white copper, as well as various types of steel and stainless steel materials, Ni strips, cold-rolled steel, strip steel (including pre-plated), galvanized sheets, low-carbon steel, spring steel, and other composite materials.
Precision sheet metal manufacture
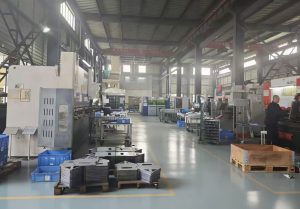
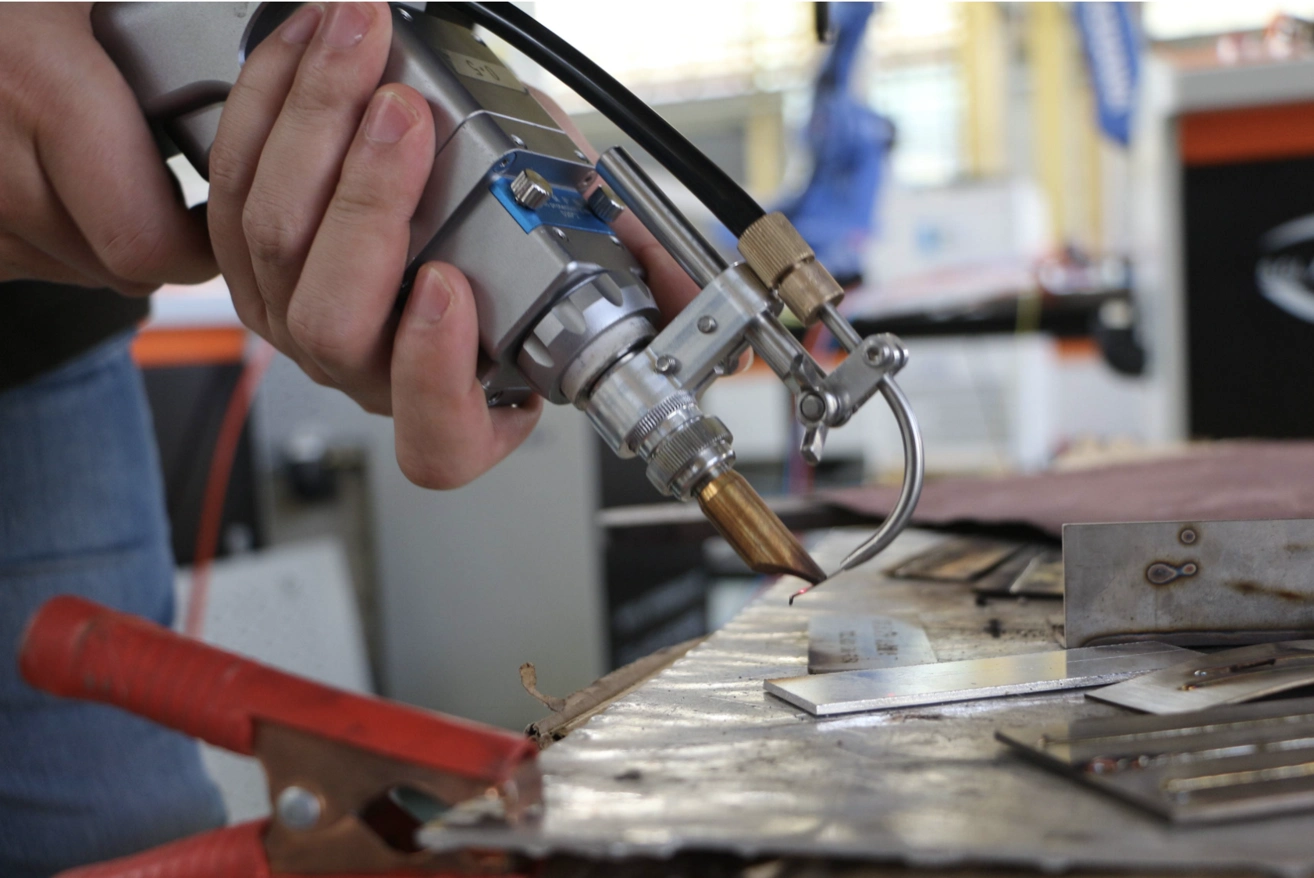
The sheet metal workshop is equipped with precision sheet metal processing equipment, including 2 large-scale advanced CNC laser cutting machines, 1 CNC punch press, 5 CNC bending machines, as well as riveting machines, welding machines, grinders, wire drawing machines and other equipment.
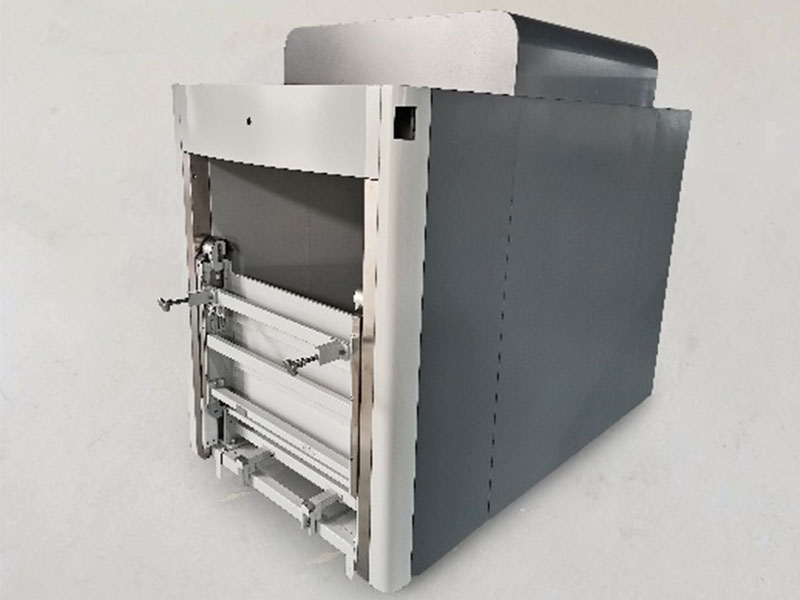
The processed products cover industrial automation, medical equipment, electrical equipment, electrical boxes, electrical junction boxes and other fields. It can perform precision processing such as rapid cutting and sheet metal processing on the following metal materials: stainless steel, carbon steel, silicon steel, aluminum alloy, galvanized sheet, aluminum-zinc plated sheet, etc.
Powder Coating & Painting
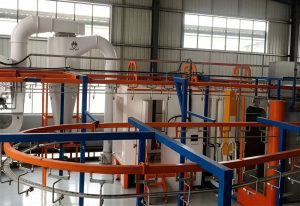
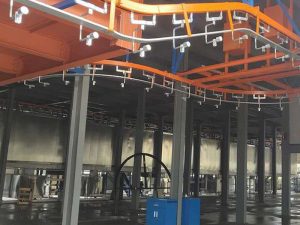
One automatic powder coating line;
One manual powder coating line (for large parts and large boxes);
One manual painting line (for large parts and large boxes);
One automatic powder coating and painting hybrid line under construction.
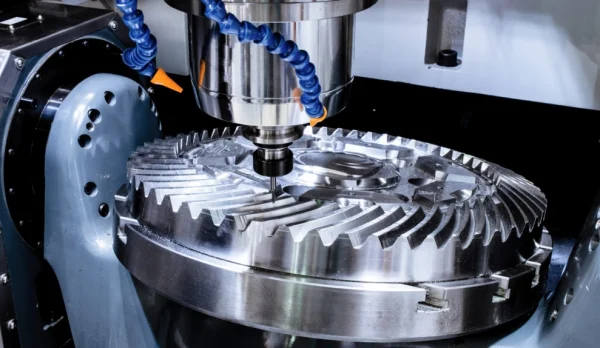
Precision machining
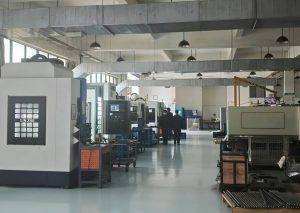
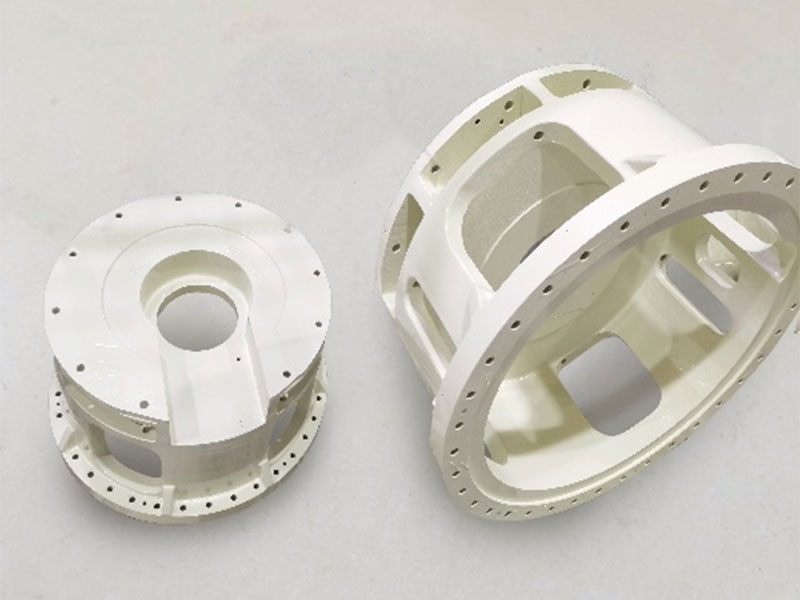
The machining workshop is equipped with precision equipment, including 6 sets of 4-axis CNC machines, 1 set of 5-axis swiss-type lathe, 13 sets of precision CNC lathes, 4 sets of CNC milling machines, 16 sets of Taiwan Mingyang precision automatic lathes, as well as precision ordinary lathes, precision 3-axis digital display milling machines, precision bench lathes, Taiwan Jizuan automatic edge milling machines, precision thread rolling machines, thread rolling dies, precision tapping machines, precision drilling machines, precision Taiwan digital display milling machines, precision knife grinders, internal and external cylindrical grinders, centerless grinders, sawing machines, ultrasonic cleaning and drying machines, polishing machines, electric welders, arc welders and other equipment.
our
Intro video
our fun facts
No more coordinating 5 + suppliers. Cost - Smart Production : Vertical integration + process optimization = 15 - 30% cost reduction vs. fragmented supply chains.
Speed-to-Market:Concurrent engineering cuts lead times by 40%. Meet deadlines without compromising quality.
Request a Free DFM Analysis:Upload your drawings/samples. Our engineers will identify cost & efficiency optimizations within 48 hours.
the company is built
0
registered capital
0M
staff
0+
factory area
0+
our case
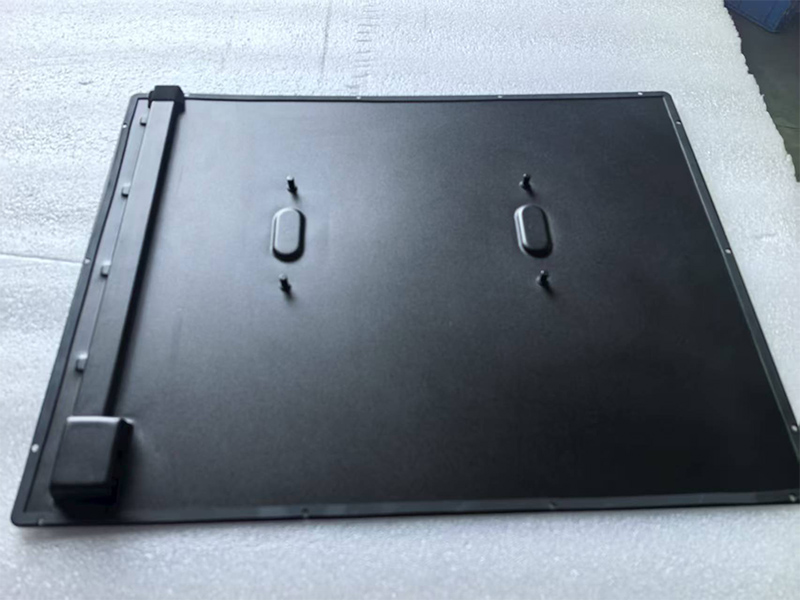
Use Stretching process Substitute for Weld+Polish +Scrape putty Technology
Use Stretching process Substitute for Weld+Polish +Scrape putty Technology
Break through the technical bottleneck and create high-quality and price-price metal structural parts for teaching demonstration equipment:
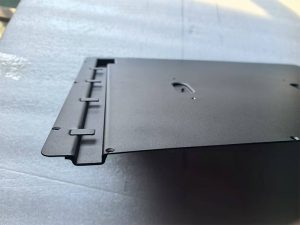
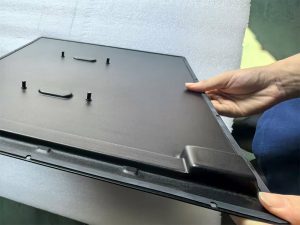
When a customer was developing a large demonstration computer for training and teaching, its core metal structural parts encountered serious challenges. The initial design of the part uses the welding process to make the protruding part, but in the product testing stage, the poor welding tightness makes the product unable to pass the key test. At the same time, the high cost of the welding process makes the price of the parts significantly higher than that of competitors, the project delivery is imminent, and customers face great pressure of quality and cost.
Accurately locate pain points and respond quickly to tackle them:
After understanding the customer’s plight, we quickly set up a special technical team. In the first technical seminar, we deeply analyzed the root cause of poor welding airtightness. Although by optimizing welding parameters and introducing welding machinesPeople, we have successfully solved the problem of airtightness and met the initial quality requirements of customers, but the problem of high welding cost is still pending.
Innovative plan, two-proged:
The technical team didn’t stop there. After many rounds of internal discussion and close communication with customers, we have proposed a fundamental solution: replace the original welding with an integrated stamping and stretching process.+Polish+Scrape putty Craft. This not only completely eliminates the risk of welding tightness from the source, but also significantly reduces the production cost and provides the possibility for the product to win a larger market space.
Seize”Impossible”, fulfill the promise:
Customer feedback has considered stamping.StretchingThe plan, but other suppliers said it could not be realized. In the face of questioning, we firmly believe that”One learns by doing”. Based on the profound accumulation of technology, we provide customers with key optimization suggestions, including:
Adjust the tensile slope angle to optimize the material fluidity, and choose a specific brand of cold-rolled steel plate with better tensile performance.
Excellent results, praised by customers:
After the plan was determined, we conducted multiple rounds of rigorous process tests and sample verification. The final delivered parts perfectly meet the customer’s design requirements and performance standards. The customer was extremely satisfied with the results, and not only gave high praise:”This is the perfect product in my ideal design!”He also expressed his sincere thanks for the ability of the Chuangkai team to overcome difficult problems. We have successfully helped customers within the urgent delivery period, while solving difficult quality and cost problems, and helping their products gain an advantage in market competition.
OvercomiNg Technical Hurdles to Deliver High-Quality, Cost-Effective Metal Components for Educational Displa And Systems
The challenge:
A client developing large demonstration computers for training and education faced Critical iss Ues with a key metal structural component. The initial design utilized welded protrusions. However, during product testing, poor weld sealing integrity caused failures. Compounding the problem, the high cost of the welding process made their component signIficantly more expensive than competitors’. With project deadlines looming, the client was under immense pressure to resolve both quality and co St challenges.
Our Rapid Response & Initial Solution:
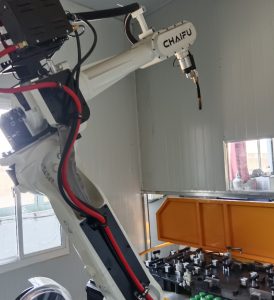
Upon learning of the client’s dilemma, we imMediately formed a dedicated technical task force. In the initial technical review, we thoroughly analyzed the root cause of the sealing failure. Through extensive welding parameter optimization trials and the strategic implementation of roboticWelding, we successfully achieved the required sealing integrity, meeting the client’s quality speci Fications.
Identifying the Deeper Issue & Proposing Innovation:
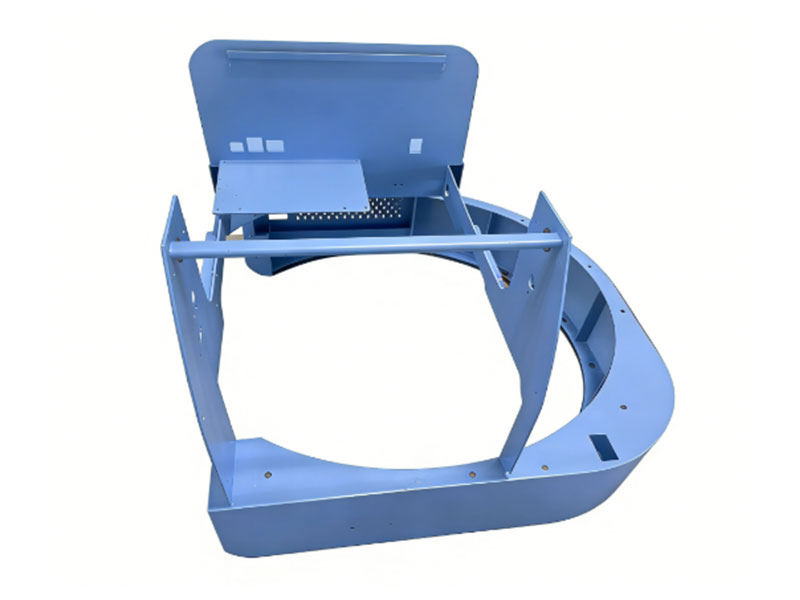
While the immediate sealing issue was resolved, the fundamental problem of prohibitive manufacturing Costs remained. Refusing to settle, our task force engaged in intensive internal brainstorming and maintained close Communication with the client. We proposed a transformative solution: replace the welded assembly with a single-piece component foRmed by stamping and deep drawing.This approach promised to:
- Eliminate the root cause of sealing failures inherent in welding.
- Achieve significant cost reduction By streamlining production.
- EnHance market competitiveness** for the client’s end product.
Breaking Through the “Impossible”:
The client revealed they had previously explored stamping, but other suppliers deemed it unfeasible For this part. Guided by our belief that”Proof lies in practice,” we leveraged our technical expertise to propose crucial design optimizati Ons:
- 1Adjusting the draw angle to improve material flow.
- 2Specifying a higher-grade cold-rolled steel with superior deep-drawing properties.
The Successful Outcome:
After rigorous prototyping and validation testing based on our optimizeD design, we delivered the final component. The results were exceptional, perfectly aligning with the client’s design intent and performance req Uirements.The client expressed deep satisfaction, offering high praise: “This is the perfect product I en Visioned in my design!” They explicitly thanked ChuangKai for solving their persistent technical headache. We enabled the client to meet their critical deadLine while simultaneously overcoming both the quality defect and the cost barrier, significantly enh AnCing their products’s market competitiveness.
Case Study on Improvements for Agricultural Machinery Shaft Breakage
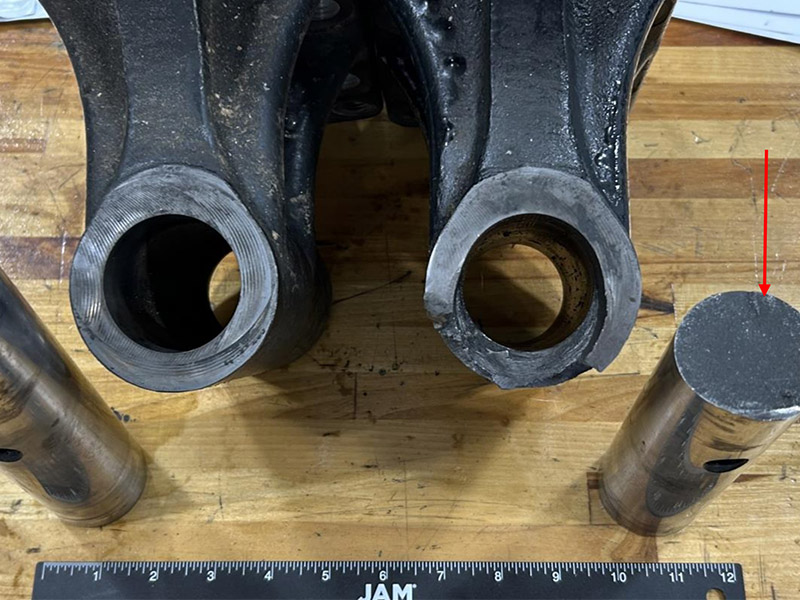
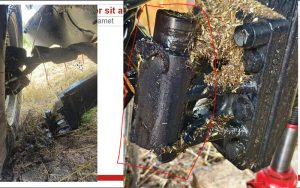
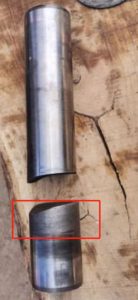
In July 2024, a customer gave feedback that Theirs The axis of the combine harvester There was a rupture during the field operation, and the end customers were very anxious about the fact that the ripe grain could not be harvested smoothly. They initially thought that it might be the raw material of the shaft 40CrNiMoA or the heat treatment process that did not meet the requirements. We have received Their help the broken axis was analyzed at the first time, and it was concluded that it was not Raw materials and There is a problem with the process, but it is designed by the customer.SeasonIt is not taken into account the complex working conditions of the equipment.And one-way force fatigue Hidden dangers, customer requirements Whole Tall Hard Degree heat treatment leads to the high hardness of the core, which is easy to produce Tired Break,After analysis We suggest adopting Whole Adjust the quality plus Surface The process of induction quenching replaces the original heat treatment Overall high hardness The process makes the core Hardness Reduce And the outer surface hardness is high, which meets the wear resistance., and sent it to the customer according to the suggested process.The new sample achieved excellence in the second field experiment.Bear fruit The feedback of.
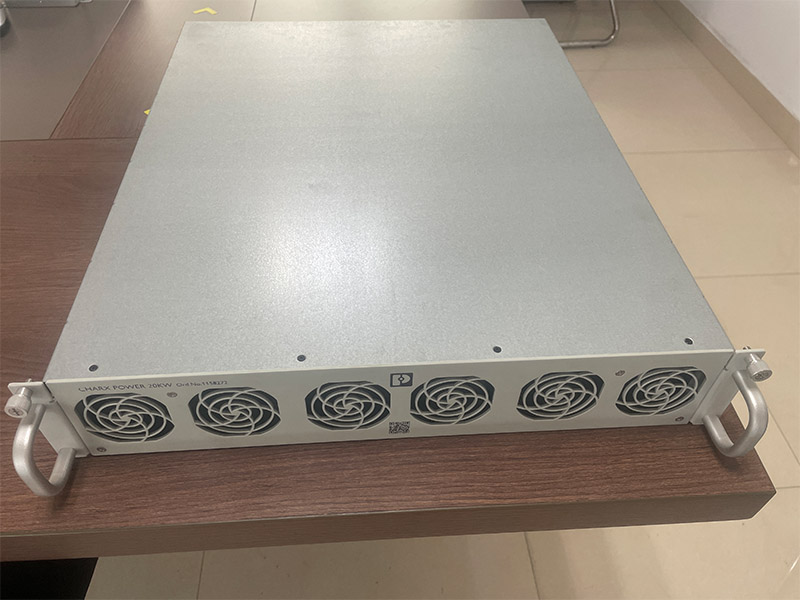
Power supply box enclosure improvement process
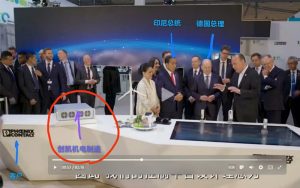
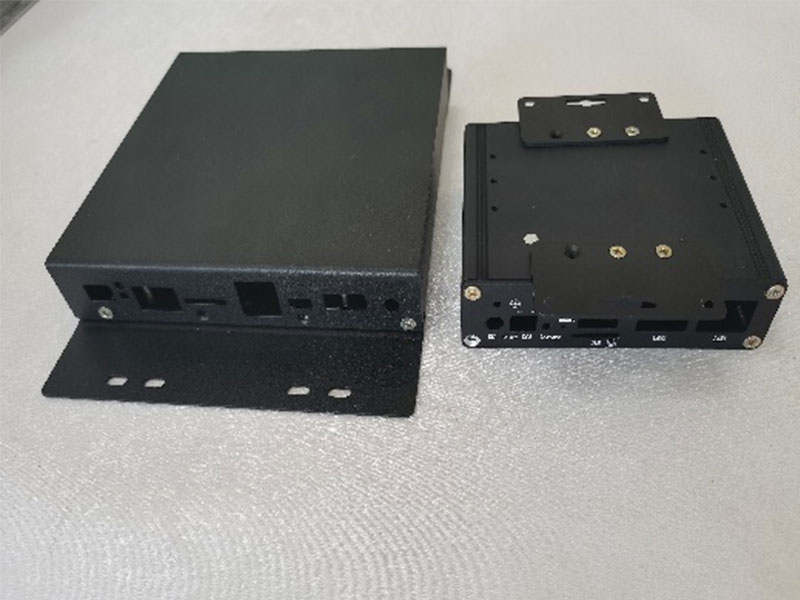
A German customer of our company has a combination box that has difficulty in the design stage. If the riveting method is adopted, it will protrude from the plane to affect the function. If the welding method is used, the appearance does not meet the requirements and the cost is high. After contacting us, we happened to have successful cases in other projects. We can solve customer problems very well by using double flat head rivets and salad holes. We sent samples to customers.
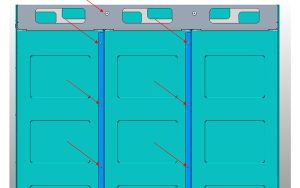
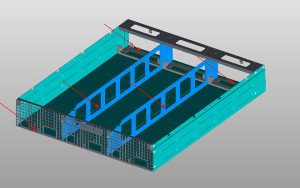
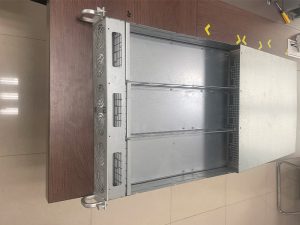
They were very satisfied and achieved rich results at the Hanover exhibition.,AchieveUnanimous praise!
Your End-to-End Manufacturing Solution Partner
Your End-to-End Manufacturing Solution Partner
From Concept to Completion – Precision Engineered for Global Success
At ChuangKai, we eliminate the complexities of multi-vendor sourcing. As a vertically integrated manufacturer specializing in ODM & OEM solutions, we deliver seamless production of high-precision components through our comprehensive capabilities:
Integrated Manufacturing Services:
- Machining: CNC Milling/Turning, Swiss Machining
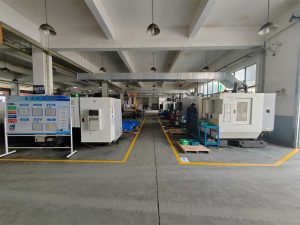
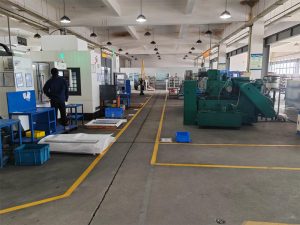
- Metal Fabrication:Laser Cutting, Bending, Welding
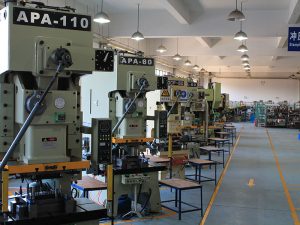
- Stamping & Forming: Progressive Die Stamping, Deep Drawing
- Tooling & Molding:Custom Die/Mold Design & Manufacturing
- Surface Treatment: Powder Coating, Spray Painting
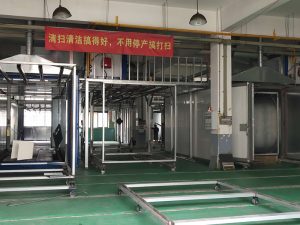
- Assembly & Testing:Full Kitting, Quality Validation
ODM/OEM Advantages for Your Business:
Design Innovation
Our engineering team collaborates with you to optimize designs for manufacturability, cost-efficiency, and performance – transforming concepts into market-ready products.
Single-Source Accountability
No more coordinating 5+ suppliers. We manage the entire workflow under one roof:
Design → Prototyping → Tooling → Raw Material Sourcing → Production → Finishing → Assembly → Logistics
Cost-Smart Production
Vertical integration + process optimization = 15-30% cost reduction vs. fragmented supply chains.
| Speed-to-Market |
Concurrent engineering cuts lead times by 40%. Meet deadlines without compromising quality.
| Quality Built-In |
ISO-certified processes with digital traceability. PPAP, FAIR, and CPK reporting available.
√ Industries We Serve:
Automotive | Industrial Machinery | Medical Devices | Renewable Energy | Robotics | nuclear electricity generation
Why Global Clients Choose Us:
Problem Solvers:Like the [Teaching Demonstration Equipment Case] where we replaced welded assemblies with integrated stamped parts –solving leaks + cutting costs 25%.
Scalable Capacity:Support from NPI prototypes to 1M+ unit production runs.
Technical Agility: 20+ engineers ready to tackle complex GD&T, tight-tolerance (±0.01mm), and material challenges.
→ Request a Free DFM Analysis
Upload your drawings/samples. Our engineers will identify cost & efficiency optimizations within 48 hours.
Products
FAQ
This section answers common questions about our mechanical and electrical products, services, and policies. It helps you quickly find information without contacting support
Our core strength lies in integrating the entire industrial chain, from precision machining, precision sheet metal processing, stamping production, tolling design and manufacturing, professional surface treatment by spraying to final product assembly, and implementing an outstanding quality management system throughout the entire process. This means that customers do not need to coordinate multiple suppliers to obtain efficient, coordinated, and consistent services. Our strict quality control is implemented in every link, ensuring that what is ultimately delivered is not only parts or products that meet requirements, but also stable, reliable, and high-standard overall solutions, effectively helping customers shorten delivery times, reduce costs, and improve supply chain efficiency.
Customized non-standard component processing. This depends on the complexity of the product. The general delivery period is usually between 2 and 4 weeks.
25
Years Experience
Contact us
recent articles
recent articles
Need mechanical and electrical solutions or have questions? Get in touch!
Robot Components Manufacturing Guide: CNC Machining vs Sheet Metal Fabrication vs Metal Stamping
28
August
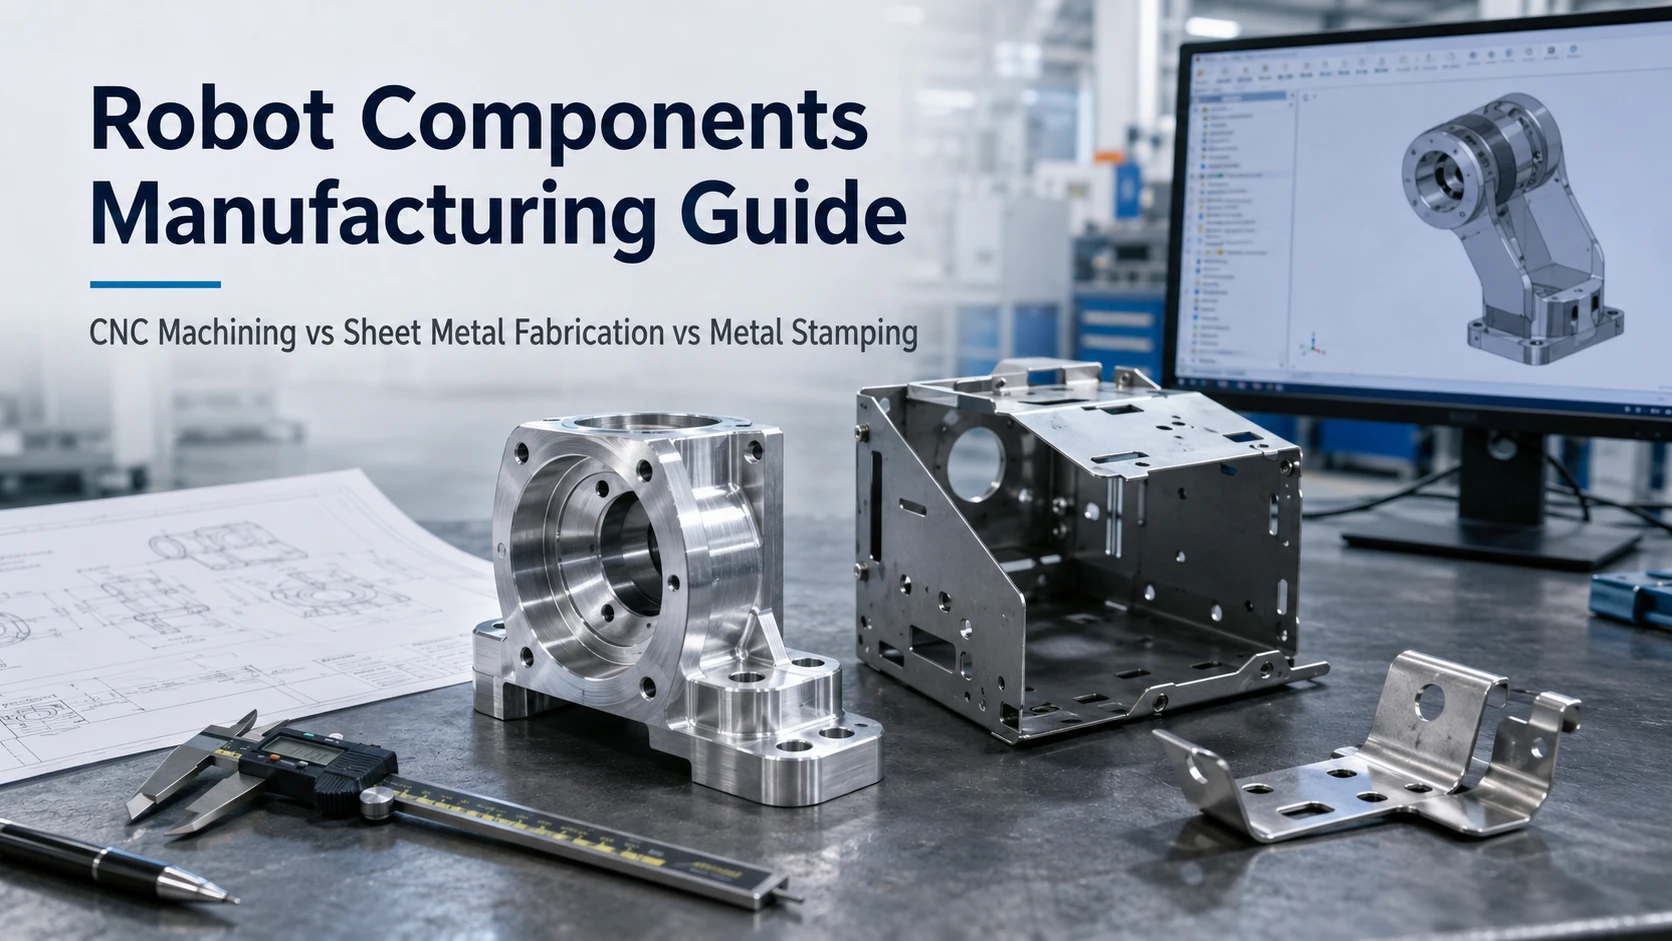
Choosing the right process for robot components manufacturing starts with the part, not the machine. A compact joint housing, a thin-wall chassis, and a repeat-production clip may belong to the same robot but require different manufacturing routes. Engineers and sourcing teams should compare geometry, stock form, critical interfaces, design maturity, production demand, secondary operations, and inspection needs before choosing CNC machining, sheet metal fabrication, metal stamping, or a hybrid process.
CNC Machining vs Sheet Metal vs Stamping for Robot Components: How to Choose
Start by asking whether the part is fundamentally a solid three-dimensional component, a fabricated sheet structure, or a thin repeatable formed part. Then review precision, design stability, and expected demand. CK Metal Tech’s existing process guidance similarly treats geometry, stock form, design maturity, critical features, and expected production demand as key process-selection inputs.
| Project condition | CNC machining | Sheet metal fabrication | Metal stamping |
|---|---|---|---|
| Solid, complex 3D geometry | Strong fit | Limited | Usually unsuitable |
| Large thin-wall chassis or enclosure | Often inefficient | Strong fit | Depends on geometry/tooling |
| Precision bores, datum faces, threads | Strong fit | May need secondary CNC | May need secondary CNC |
| Frequent design changes | Flexible | Flexible | Tooling risk |
| Stable repeat production | Review total cost | Strong for fabricated structures | Strong candidate if tooling is justified |
Start With Part Geometry and Material Form
Bar, plate, or block stock points toward machining when the component needs deep features, bearing seats, threads, several working planes, or closely related datums. A chassis, cover, enclosure, or frame made from consistent sheet thickness is usually a better sheet metal candidate. Stamping becomes relevant when geometry can be blanked, pierced, bent, formed, or drawn from sheet or coil and repeated with stable tooling. CK Metal Tech’s existing CNC-to-stamping guidance also starts by separating solid stock geometry from parts that can be produced from sheet or coil.
Then Check Precision, Design Maturity, and Production Demand
Not every dimension on a robot drawing deserves the same process capability. Bearing locations, motor interfaces, alignment datums, shafts, and sensor mounting features may control function, while covers and noncritical edges can often use more flexible tolerances.
Design maturity is equally important. CNC machining and laser cutting with bending are easier to revise while a robot design is changing. Dedicated stamping dies carry more revision risk. There is no universal production quantity at which stamping automatically becomes economical; tooling, geometry, secondary work, material behavior, and lifetime demand all affect the decision.
When Is CNC Machining the Right Choice for Robot Components?
Use CNC for Precision Interfaces and Complex 3D Components
CNC machining fits robot components that depend on controlled three-dimensional geometry, such as joint housings, shaft-related parts, motor mounting interfaces, bearing seats, machined datums, or multi-plane threaded features. It is also useful during prototype and pilot stages because design changes do not require a dedicated forming die. CK’s published process comparison identifies prototypes, changing designs, solid geometry, precision bores, threads, and datum faces as conditions that can favor machining.
When requesting CNC machining for robot components, identify functional datums and critical interfaces instead of tightening every dimension. Confirm how the workpiece will be located, which features can remain in one setup, whether grinding or finishing follows machining, and how assembly-critical geometry will be inspected.
Know When CNC Machining Becomes an Expensive Route
Machining can be inefficient when large amounts of stock must be removed to create a simple thin-wall structure. A robot enclosure, cover, or broad mounting structure may be better suited to cutting and bending if only a few areas require high precision.
In that situation, separate the base structure from the precision interfaces. A fabricated or stamped body can create most of the geometry while CNC is reserved for bearing bores, datum faces, threads, or other critical features. CK’s current process guidance also recognizes stamped-base-plus-machined-critical-feature routes where forming can create the main geometry but precision interfaces still require secondary work.
When Is Sheet Metal Fabrication Better for Robotics?
Use Sheet Metal for Chassis, Covers, Enclosures, Frames, and Brackets
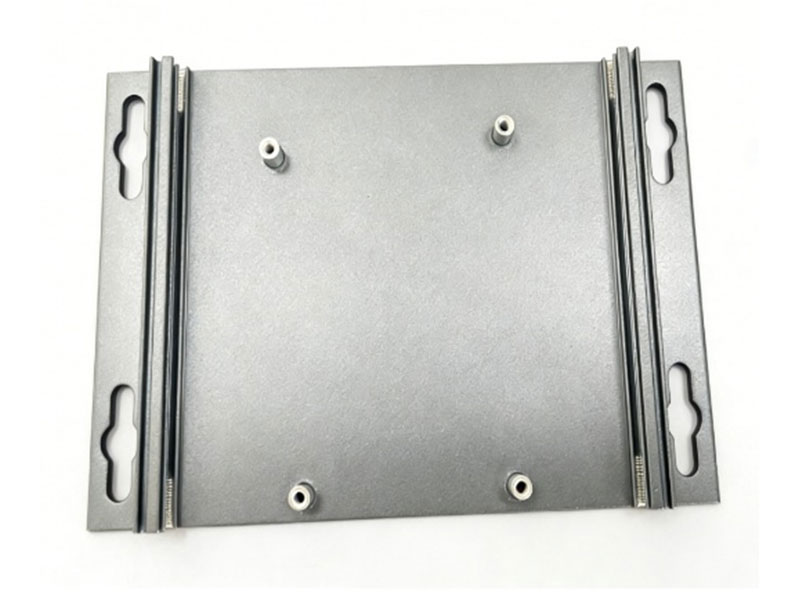
Sheet metal fabrication is a strong candidate for structures made from relatively consistent wall thickness: robot chassis, equipment covers, control enclosures, mounting frames, panels, and structural brackets. Cutting, punching, bending, riveting, and welding can build these forms without machining them from solid stock.
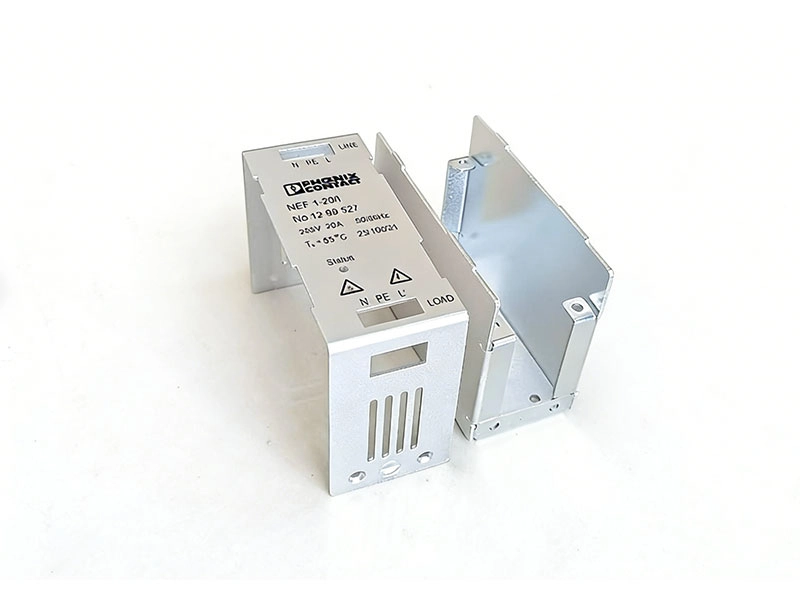
For sheet metal fabrication for robotics, define material, thickness, bend geometry, joining method, finish, critical interfaces, and assembly requirements. CK Metal Tech publicly lists laser cutting, CNC punching, bending, riveting, and welding within its sheet metal capability, and industrial automation is among the applications stated on the site.
Control Bend Accuracy, Welding Distortion, and Datum Stack-Up
A fabricated assembly can create fit problems even when its individual pieces are acceptable. Bend variation, welding distortion, tolerance accumulation, or finishing on mating areas may shift motor, sensor, or mounting interfaces.
Mark important datums before production and decide which dimensions need post-weld inspection. Fixture design, welding sequence, heat input, and early design review can affect dimensional stability in welded sheet structures. Where a bearing or motor interface must remain tightly controlled, post-fabrication machining may reduce assembly risk.
When Does Metal Stamping Make Sense for Robot Components?
Use Stamping for Thin, Repeatable, Feature-Dense Components
Metal stamping becomes attractive when a robot component uses sheet or coil, has stable geometry, and will repeat enough to justify tooling. Possible candidates include retainers, clips, shields, thin brackets, spring features, shims, sensor flags, and parts combining holes, tabs, bends, or formed details.
Stamping does not mean every feature must come directly from the die. Tapping, drilling, machining, coating, or assembly may remain necessary; CK’s published process guidance specifically notes that precision bores, threads, bearing locations, datum faces, and similar features can remain secondary operations. When evaluating metal stamping and tooling for robot components, confirm material and thickness, forming feasibility, burr-sensitive surfaces, critical dimensions, secondary operations, revision status, and expected program demand.
Do Not Commit to Stamping Tooling Before the Design Is Stable
Production tooling becomes risky when joint geometry, mounting interfaces, material thickness, or customer requirements are still changing. Late revisions can require die modification and another round of trials and sample approval.
Prototype validation and DFM should therefore happen before hard-tool release. Before tooling approval, CK’s existing guidance recommends confirming material, thickness, interfaces, critical dimensions, finish, drawing revision, and expected demand rather than relying on a fixed volume rule. Purchasing teams should also account for tooling maintenance, secondary operations, inspection, finishing, and possible modification costs.
When Is Hybrid Manufacturing Better Than a Single Process?
Combine Fabrication or Stamping With CNC for Critical Features
Robot components do not have to fit one process exclusively. A welded structure can be machined afterward to establish a motor datum or bearing interface. A stamped base can receive drilling, tapping, reaming, milling, or grinding where the functional requirement exceeds what forming should control.
A hybrid route makes sense when fabrication or stamping creates most of the geometry and a short secondary operation controls only critical features. It becomes less attractive when nearly every surface still needs machining or forming variation prevents repeatable fixturing. The same principle appears in CK’s existing CNC-to-stamping guidance, where a stamped base can be combined with secondary machining for precision features.
Common Robot Component Manufacturing Mistakes and How to Prevent Them
Avoid Over-Machining, Over-Tolerancing, and Premature Tooling
Three errors create avoidable cost: machining a thin structure from solid stock when fabrication could perform the function, applying tight machining-style tolerances to every fabricated or stamped feature, and approving production dies before the design is stable.
A useful DFM review classifies features as function-critical, assembly-critical, or noncritical. It then matches each feature to the stock form and manufacturing process that creates it most naturally. Precision machining or special inspection should be reserved for requirements that affect performance or assembly.
What Should Be Included in a Robot Components Manufacturing RFQ?
Give the Supplier Enough Information to Recommend the Manufacturing Route
Send the current 2D drawing and STEP model, material and stock form, part function, critical datums and tolerances, prototype quantity, expected repeat demand, finish, inspection requirements, mating components, assembly conditions, and revision status. For tooling projects, state expected program demand and whether the design is frozen. CK’s published sourcing guidance similarly calls for current drawings, STEP files, material, quantities, critical tolerances, secondary operations, finishing, and inspection requirements when comparing routes.
Also identify where process changes are acceptable. This gives the supplier room to propose a fabricated body with machined datums or move a stable thin component toward stamping without changing the functional requirements.
How to Choose a Robot Components Manufacturing Supplier
Compare Process Selection, DFM, Inspection, and Multi-Process Capability
A supplier should explain why the proposed process fits the component and what would justify a different route. Compare DFM feedback, material capability, tooling responsibility, machining and forming resources, secondary finishing, inspection planning, revision control, and assembly coordination—not only unit price.
CK Metal Tech lists machining, sheet metal processing, metal stamping, tooling design and manufacturing, surface finishing, and component assembly within its integrated precision metal manufacturing capabilities. That combination is relevant when one robot assembly contains machined interfaces, fabricated structures, stamped parts, and secondary operations that must work together.
The actual drawing still controls the decision. CK Metal Tech should be evaluated against the component’s geometry, tolerances, volume, finish, inspection, and assembly requirements rather than a capability list alone.
Conclusion
Robot components manufacturing works best when process selection follows geometry first, then critical precision, design maturity, production demand, and secondary operations. CNC suits many solid and precision-interface components; sheet metal fits many chassis, covers, frames, and brackets; stamping suits stable repeat formed parts; and hybrid routes can combine them.
For a process review, prepare the drawing, 3D model, material, critical dimensions, application, finish, prototype and production quantities, and inspection needs. Buyers can contact CK Metal Tech to discuss manufacturability without assuming that one process is automatically the right choice.
FAQs About Robot Components Manufacturing
Which robot components are usually CNC machined?
Parts with complex 3D geometry, precision bores, threads, bearing locations, motor interfaces, or important datum relationships are common CNC candidates. Material, tolerances, quantity, and secondary requirements still need review.
Is sheet metal fabrication suitable for robot chassis and enclosures?
Yes, when the structure uses relatively consistent sheet thickness and can be cut, bent, riveted, or welded. Precision motor or bearing interfaces may still require secondary machining.
When should a robot component move from CNC or laser cutting to stamping?
Consider stamping when the geometry suits sheet or coil forming, the design is stable, and repeat demand can justify tooling and validation. There is no universal quantity threshold.
Can one robot component use both stamping and CNC machining?
Yes. Stamping can create the base geometry while machining, drilling, tapping, reaming, or grinding completes critical interfaces. The hybrid route should be evaluated as a complete manufacturing process rather than by press cost alone.
Battery Management System (BMS) Enclosure Design Guide: Materials, IP Sealing, EMI Shielding & Thermal Management
27
August
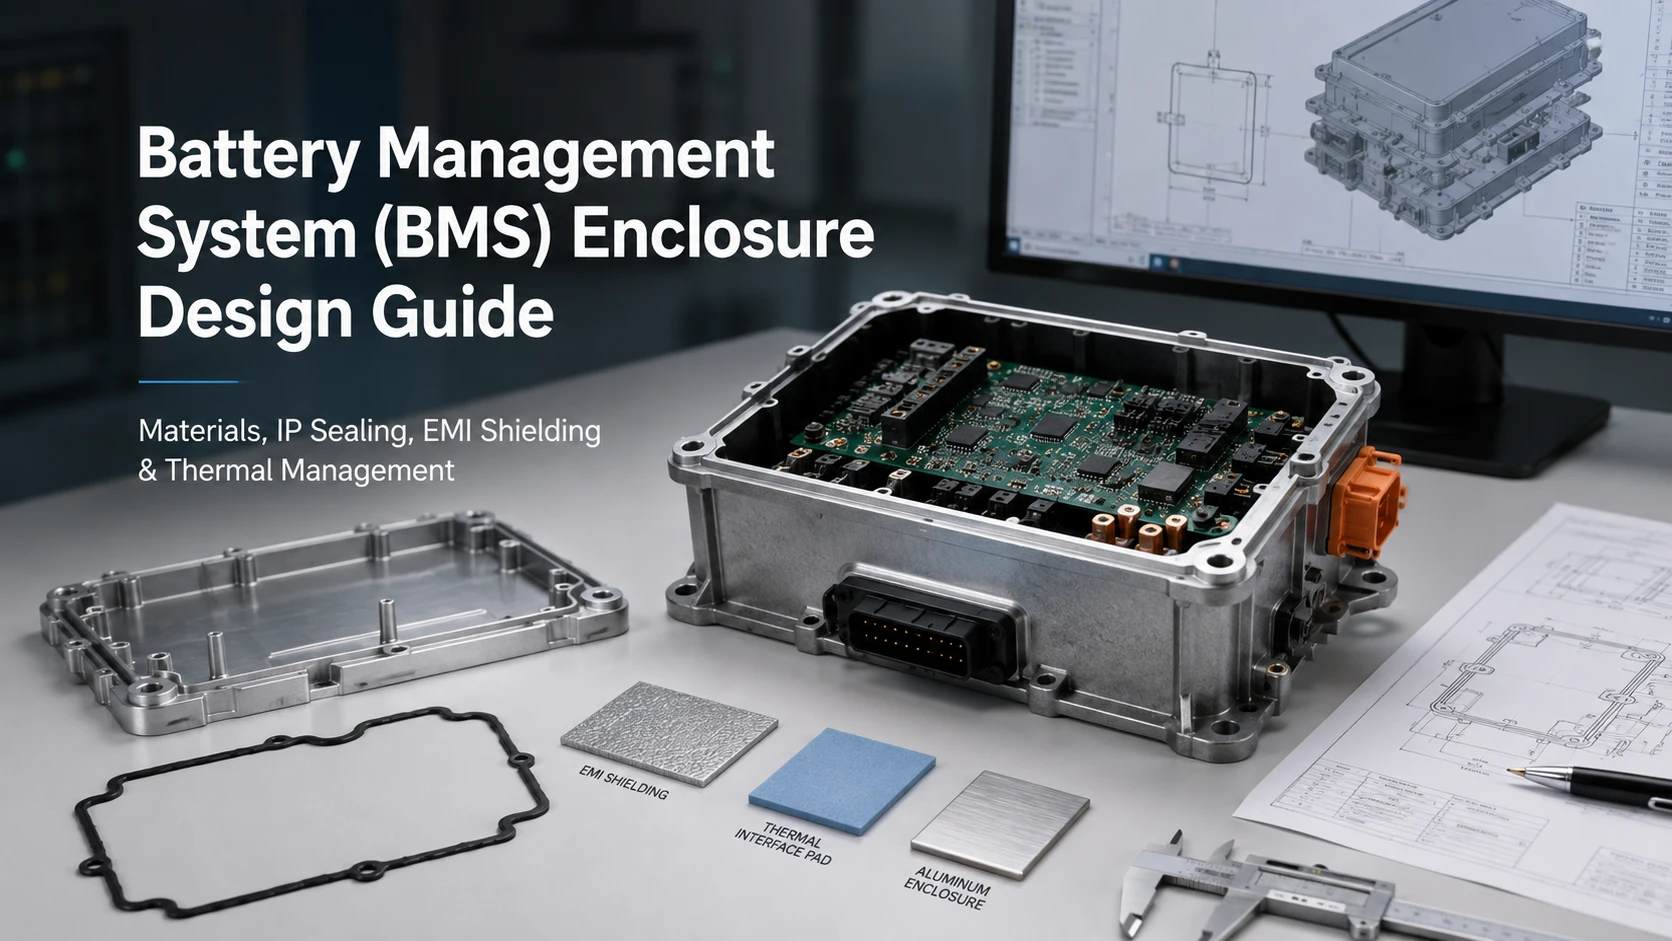
A good BMS enclosure design must protect electronics without creating problems in sealing, EMI, heat dissipation, assembly, or repeat production. For EV and energy storage projects, define the operating environment first, then select the material, sealing concept, grounding strategy, thermal path, and manufacturing route.
What Should You Define Before Designing a BMS Enclosure?
Define the Application, Environment, and Mechanical Requirements First
Start with installation conditions. Confirm whether the battery management system is used in a vehicle, stationary energy storage equipment, or another industrial application, then define water and dust exposure, vibration, temperature, service access, PCB envelope, mounting points, connectors, and cable routing. IEC 60529 classifies enclosure protection under the IP Code, so an IP target is a project requirement to verify, not a generic feature of every metal housing.
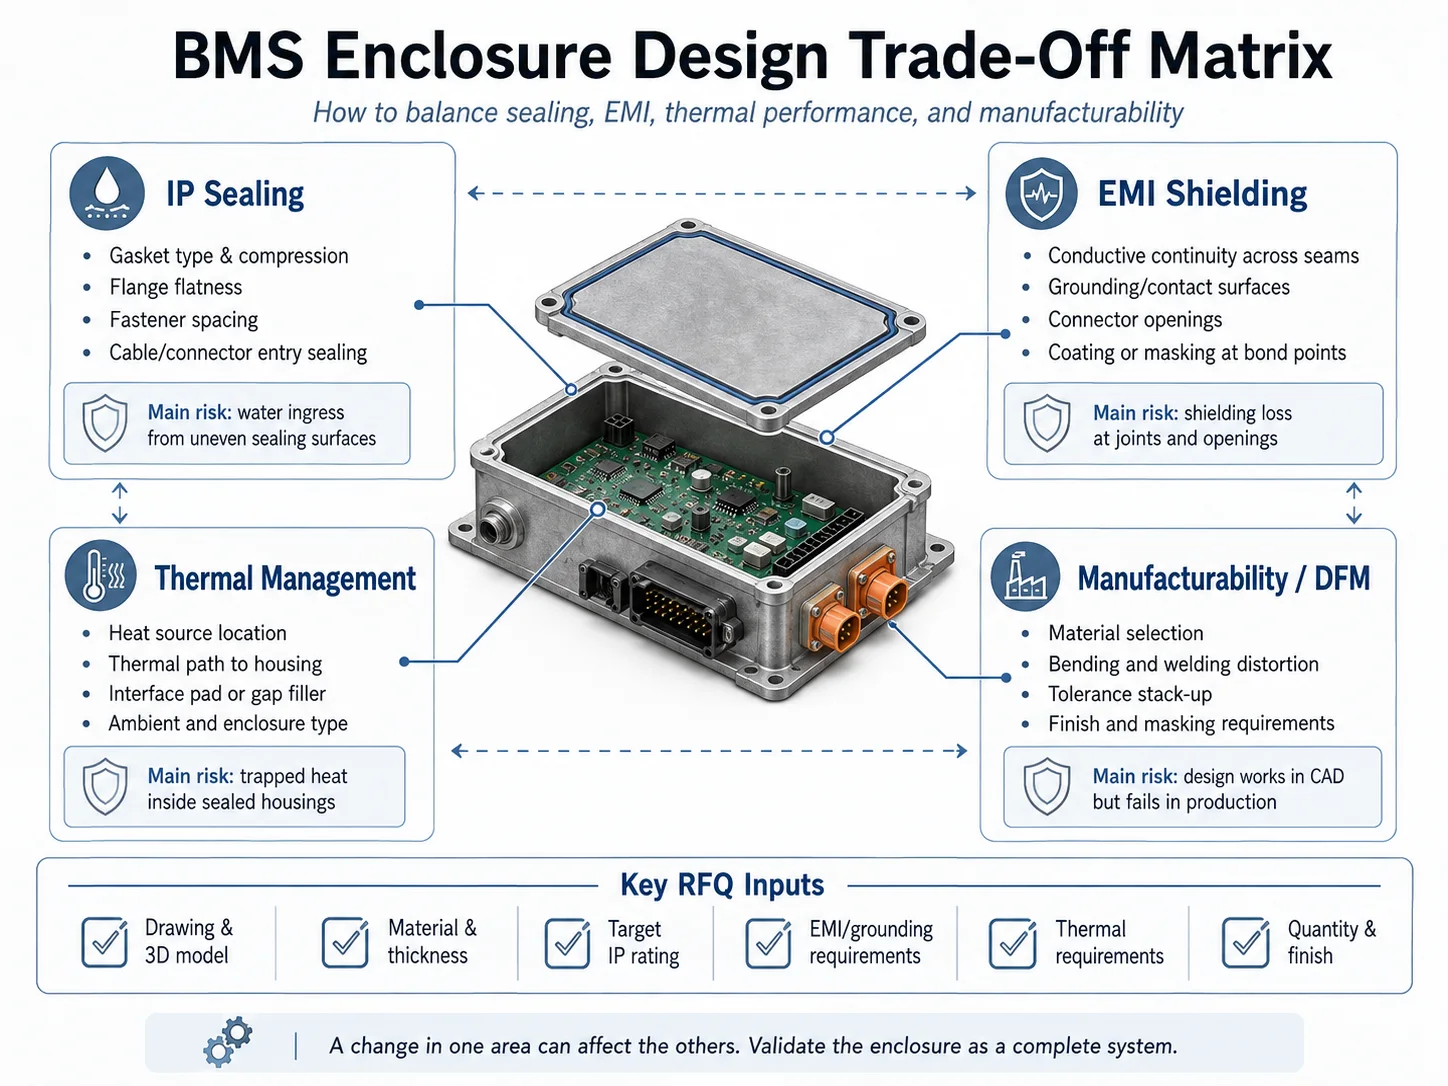
Before CAD release, review likely failure modes: water ingress, EMI leakage, trapped heat, connector misalignment, weld distortion, and coating on functional contact surfaces. Convert each risk into a drawing note, inspection point, or validation requirement.
How to Choose the Right BMS Enclosure Material
The confirmed BMS enclosure offering includes AL5052, AL6061, and SECC. Selection depends on geometry, forming, weight, corrosion exposure, grounding, thermal behavior, finish, and cost.
| Decision factor | AL5052 | AL6061 | SECC |
|---|---|---|---|
| Typical fit | Formed sheet-metal housing | Machined or more rigid features | Steel sheet-metal housing |
| Weight priority | High | High | Lower |
| Forming focus | Often favorable | Check temper and geometry | Often favorable |
| Key RFQ check | Temper, thickness, finish | Temper, machining/forming route | Coating and corrosion requirement |
AL5052 vs AL6061 vs SECC: Which Fits the Project?
AL5052 is commonly selected where formability and corrosion resistance matter. AL6061 is widely used in engineering applications where strength, machining, and structural features are important. Electrogalvanized steel provides another route where steel stiffness, forming, conductivity, and corrosion protection are useful. Primary producers describe these material families in similar terms.
For procurement, specify grade, temper where relevant, thickness, finish, and whether alternatives may be proposed. Check substitutions against bending, joining, grounding, thermal, and finishing requirements.
If coating or anodizing is planned, mark sealing faces, grounding zones, threads, and mating surfaces on the drawing. The related powder coating for sheet metal enclosures guidance is useful because coating buildup on functional interfaces can create assembly problems rather than cosmetic defects.
How to Design BMS Enclosure Sealing and IP Protection
Why BMS Enclosures Leak
Leakage may start with flange distortion, uneven closure force, poor surface condition, connector penetrations, or incorrect gasket compression. Welding matters because a housing can look acceptable while the sealing face has moved out of flatness.
Before prototype release, review flange geometry, lid stiffness, fastener spacing, gasket retention, connector openings, cable entries, and changes caused by welding or coating. Parker enclosure examples show that mating geometry, surface condition, seal installation, and compression can affect leak performance.
How to Specify Gaskets, Flanges, Fasteners, and Cable Entries
Gasket selection depends on environment, mating materials, flange geometry, closure force, chemical exposure, service cycle, and whether EMI shielding is also required. An environmental seal and a conductive EMI gasket are not automatically interchangeable. Parker Chomerics distinguishes EMI/grounding gaskets that do not provide a weather seal from conductive elastomers that can combine shielding and environmental sealing.
For the RFQ, define the target ingress requirement, seal location, gasket space, fastener layout, connectors, cable entries, and validation method. A gasket alone does not make a BMS enclosure “IP67”; the completed assembly must meet the specified requirement.
How to Control EMI Shielding and Grounding in a BMS Enclosure
Where EMI Shielding Fails: Seams, Openings, and Coated Contact Surfaces
A metal enclosure is not automatically an effective EMI shield. Seams, slots, connectors, and poorly bonded joints can interrupt current continuity. Parker Chomerics notes that gaps or slots can allow electromagnetic fields through a shield unless current continuity is maintained across them.
Surface treatment is therefore part of the EMC discussion. If a lid, panel, or grounding point requires electrical contact, coating or anodizing may need masking or another engineered contact method. Mark those areas on the drawing and validate the finished enclosure, not only the bare-metal prototype.
When to Use Grounding, Bonding, or Conductive EMI Gaskets
Grounding and bonding create intentional electrical paths; EMI gaskets can maintain conductive continuity across joints. Selection should consider shielding targets, compression, flange design, environmental sealing, and corrosion compatibility. Parker describes grounded metallic shields and conductive interfaces as methods for controlling electrical noise and EMI.
Before requesting a quote, obtain EMC requirements from the electrical team. Identify grounding points, contact surfaces, connector interfaces, and whether the same joint must also provide a weather seal. This reduces unnecessary gasket cost and redesign after EMC testing.
How to Manage Heat in a Sealed BMS Enclosure
Why Sealed BMS Enclosures Overheat and How to Build the Heat Path
Increasing environmental sealing can reduce natural airflow, so the first thermal question is whether heat-producing components have a controlled path to a surface that can reject heat. Map the route from the component through the PCB or interface material to the enclosure wall, then evaluate it under the expected mounting and ambient conditions.
Thermal pads or gap fillers may help where components cannot make direct contact with the housing. Henkel describes thermal gap fillers as materials used to couple heat-producing devices to an adjacent metal case or heat sink, especially across irregular gaps. Selection still depends on gap size, assembly stress, dielectric needs, serviceability, heat load, and allowable temperature. Those inputs should come from the electrical or thermal design.
How to Prevent BMS Enclosure Problems With DFM
Control Flatness, Tolerances, Welding Distortion, and Surface Masking
A housing may fit in CAD and fail after bending, welding, riveting, or coating. Prioritize sealing-face flatness, connector position, PCB mounting, grounding surfaces, and assembly stack-up; tight nonfunctional tolerances can add cost without reducing risk.
CK Metal Tech’s sheet-metal capability includes laser cutting, CNC punching, bending, riveting, welding, grinding, and related processes, with aluminum alloy and galvanized sheet among the listed materials. Early sheet metal enclosure fabrication review is therefore useful when a BMS housing combines sealing faces, welded joints, masked electrical contacts, and finished assembly interfaces. The supplier should identify distortion, bend-access, joining, coating, and inspection risks before production tooling or fixtures are committed.
What to Validate Before Moving From Prototype to Production
Prototype approval should cover more than appearance. Check PCB and connector fit, lid closure, gasket contact, critical dimensions, grounding interfaces, thermal behavior, finish condition, and any project-specific ingress or EMC tests. If a revision changes a flange, connector, fastener, coating, or thermal contact, repeat the validation affected by that change.
For projects moving into sourcing, CK Metal Tech’s custom BMS enclosure route is confirmed for EV and energy-storage applications and uses CNC punching, bending, riveting or welding, and anodizing or spray coating. Production release should follow an agreed DFM and inspection plan rather than visual sample approval alone.
What Should You Include in a Custom BMS Enclosure RFQ?
Send enough information for suppliers to quote the same scope: 2D drawings and 3D models, revision level, application, material and thickness, finish, critical dimensions, prototype quantity, target production quantity, and assembly requirements. Add the sealing/IP target and test method, EMI or grounding contact zones, thermal interfaces, connector details, and masked surfaces.
If a requirement is still open, identify it instead of letting the supplier assume. Buyers can review precision metal manufacturing and assembly solutions when a project combines cutting, forming, welding, finishing, machining, or assembly. CK Metal Tech publicly lists these integrated capabilities.
How to Choose a BMS Enclosure Manufacturer
Compare DFM, Fabrication, Finishing, and Validation Capability—not Price Alone
A low unit price has little value if the enclosure later needs rework. Compare suppliers on drawing review, material capability, forming and joining, finishing, inspection, revision control, and communication.
CK Metal Tech positions its manufacturing scope around precision sheet metal, stamping, machining, surface painting or powder coating, and assembly. For a BMS enclosure, the practical question is whether the supplier understands how these processes interact with sealing, EMI, thermal, and assembly requirements.
Conclusion
A robust BMS enclosure design balances material, IP sealing, EMI continuity, thermal paths, and manufacturability. Before requesting pricing, prepare drawings, material and finish requirements, operating conditions, sealing and EMC needs, thermal inputs, target quantities, and critical inspection points. Buyers can contact CK Metal Tech with these details for a manufacturability review.
FAQs
What material is best for a BMS enclosure?
There is no universal choice. AL5052 may suit formed sheet-metal designs, AL6061 projects with machined or more rigid features, and SECC steel enclosure designs. Confirm geometry, weight, corrosion, grounding, thermal, forming, and finishing needs first.
How do I design a BMS enclosure for IP67?
First confirm that IP67 is required. Then review flange flatness, gasket design, closure force, fasteners, connectors, cable entries, weld distortion, and finished surfaces. The completed enclosure must be validated against the specified ingress-protection requirement.
Does a BMS enclosure need EMI shielding?
It depends on system EMC requirements. A metal housing can support shielding, but seams, openings, connectors, coatings, and weak bonding may reduce effectiveness. Define interfaces with the electrical team and verify the finished configuration.
How do I cool a sealed BMS enclosure?
Identify the heat-producing components and create a controlled path toward the enclosure or another heat-rejection surface. Interface materials may help across gaps, but confirm heat load, allowable temperatures, geometry, and operating environment first.
Telecom Enclosure Design for Future 6G Infrastructure: Thermal Management, EMC, Corrosion and RFQ Checklist
21
August
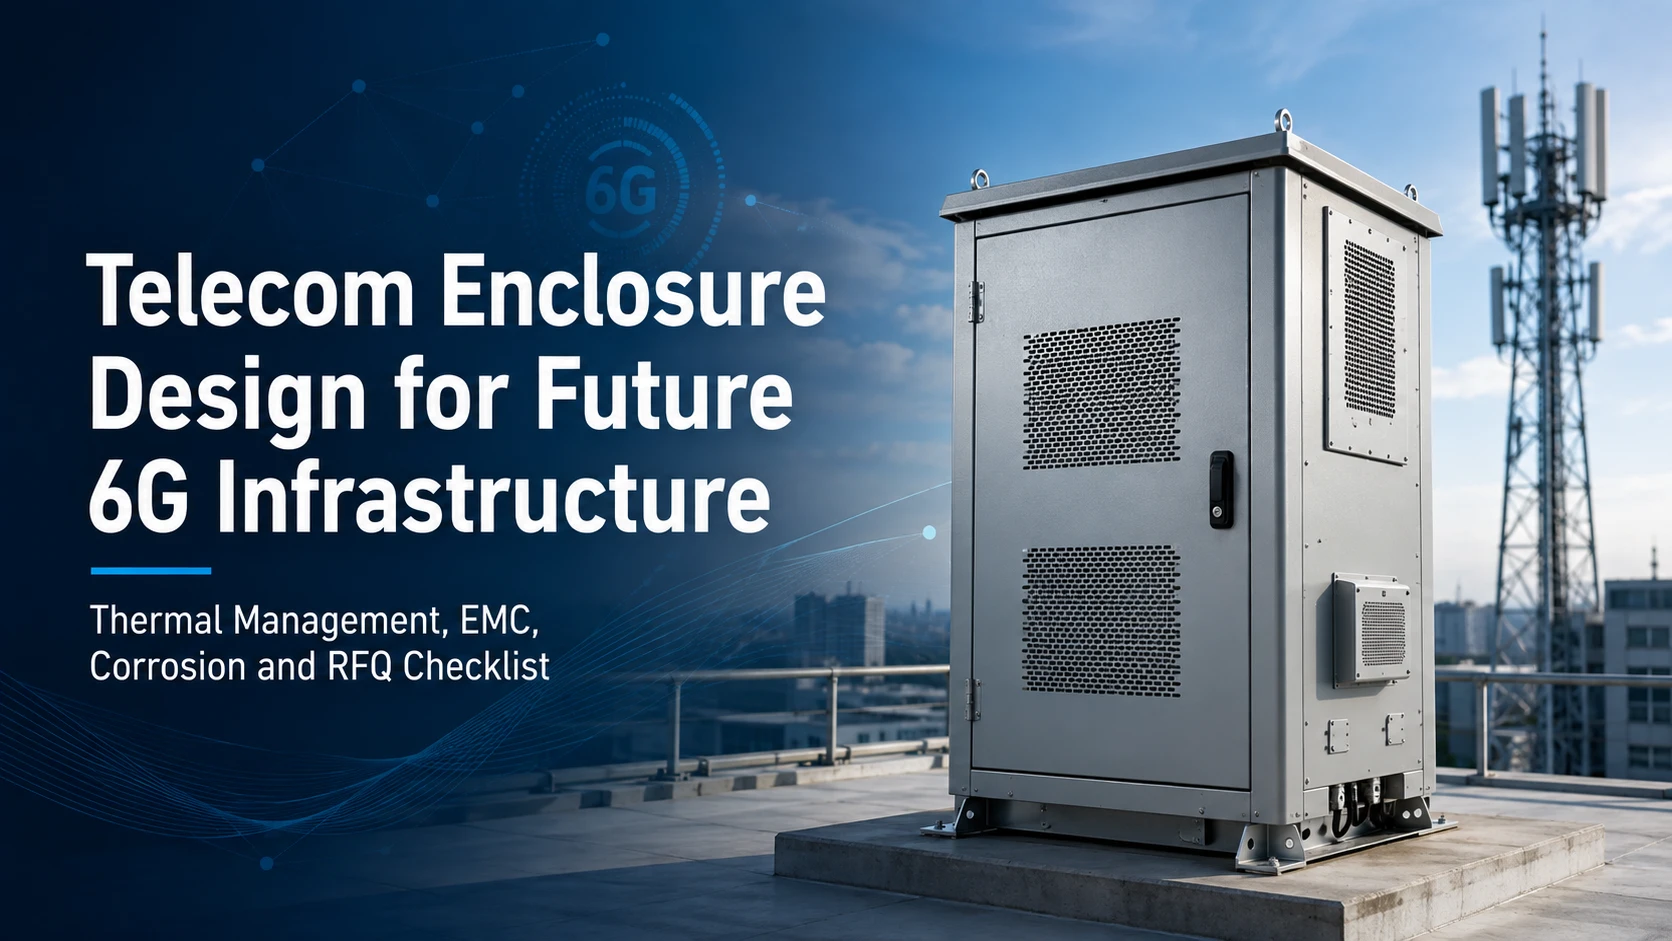
A telecom enclosure design for future 6G infrastructure should begin with equipment heat load, installation site, environmental exposure, electromagnetic compatibility, maintenance access, and manufacturing scope—not a “6G-ready” label. For equipment engineers and B2B buyers, the objective is to convert operating conditions into a buildable specification, a testable prototype, and a comparable RFQ.
What “6G-Ready Telecom Enclosure” Can—and Cannot—Mean Today
Separate Current Enclosure Requirements from Unfinished 6G Specifications
IMT-2030, the ITU framework associated with 6G, is still progressing through technical requirements, candidate technology, evaluation, and approval. Its radio-interface performance requirements do not prescribe one sheet metal material, IP rating, cooling method, or corrosion class for telecom cabinets. A product may be designed for future-generation communication equipment, but “6G compliant enclosure” is not a complete specification unless the customer defines the equipment and acceptance requirements.
A 6G network communication box enclosure can serve as a build-to-print product example, but its thermal, EMC, ingress, and corrosion performance must still be verified against the application. RFQs should replace broad future-ready claims with measurable requirements.
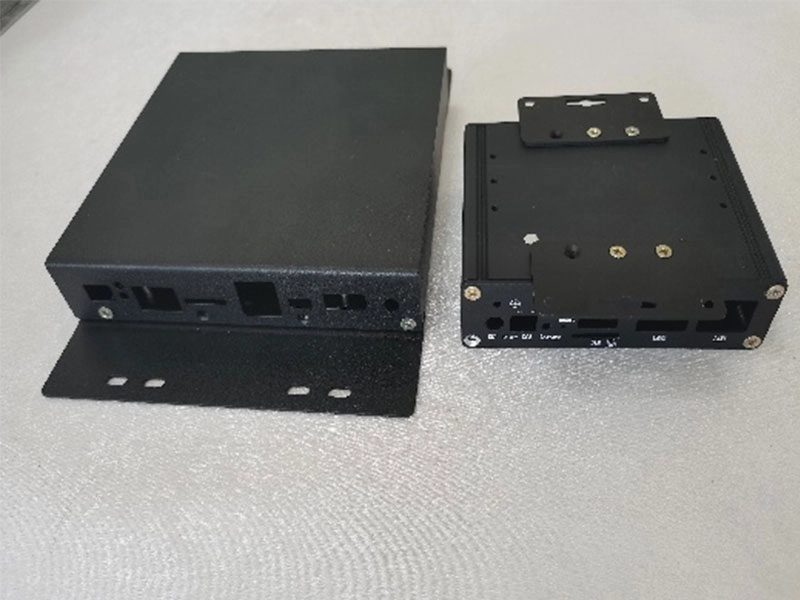
Define the Equipment, Installation Site, and Supplier Scope
Indoor boxes, outdoor pole-mounted enclosures, roadside cabinets, and weather-protected housings face different temperature, moisture, contamination, vibration, and service conditions. ETSI environmental standards classify telecommunications equipment by deployment and environmental severity, so the site should be defined before materials and tests are selected.
The OEM should provide equipment layout, heat dissipation, weight, mounting, cable interfaces, and access direction. The enclosure supplier converts those inputs into manufacturable panels, doors, joints, mounting features, and finishes. Buyers reviewing about Zhejiang Chuangkai Mechanical and Electrical Technology Co., Ltd. should distinguish confirmed manufacturing processes from project-specific performance claims.
Balance Thermal Management, Ingress Protection, and Condensation Control
Build the Thermal Input Before Selecting a Cooling Method
Cooling cannot be selected from enclosure size alone. Define internal heat dissipation, component distribution, ambient temperature limits, solar exposure, allowable internal temperature, and expected dust loading. These factors determine whether passive, ventilated, or sealed cooling is appropriate.
Open ventilation may suit a controlled indoor location but not a site exposed to rain, salt, or industrial contaminants. A highly sealed enclosure can improve ingress protection while trapping heat. The RFQ should state who is responsible for thermal analysis, prototype measurement, and approval.
Prevent Condensation Without Compromising Environmental Protection
An enclosure can resist external water and still develop internal condensation. Temperature cycling changes internal pressure, moisture may enter during maintenance, and humid air can condense on cooler metal surfaces. The risk depends on climate, sealing, shutdown cycles, internal heat, and orientation.
Possible controls include pressure-equalizing vents, drainage, internal heaters, or controlled circulation. Prototype testing should use the final door, gasket, cable glands, filters, and installed accessories. If condensation occurs, review the complete moisture and temperature path rather than assuming the gasket alone failed.
Design EMC Continuity into the Sheet Metal Enclosure
Control Seams, Doors, Panels, Gaskets, and Grounding Paths
A metal enclosure does not automatically provide adequate shielding. Electrical discontinuities can occur at doors, removable panels, hinges, painted joints, fasteners, and long seams. ETSI EN 300 386 defines EMC requirements for telecommunications network equipment, but compliance applies to the assembled equipment and its interfaces, not merely the metal housing.
Drawings should identify conductive contact areas, grounding studs, gasket locations, fastener patterns, and surfaces that must remain free of insulating coating. Conductive gaskets may suit frequently opened panels, but selection depends on frequency range, compression, environment, and maintenance.
Manage Ventilation and Cable Entries Without Creating Shielding Leaks
Ventilation openings and cable entries often become weak EMC paths. Large louvers may improve airflow but interrupt shielding continuity. Cable glands may preserve environmental sealing while still requiring bonding, filtering, or controlled placement.
Power, signal, and radio-frequency interfaces should be reviewed together with airflow and access. Powder coating can also isolate contact surfaces, so masked areas, door frames, grounding points, and fastener interfaces should be marked on the drawing. Final performance should be confirmed through system testing.
Select Materials and Corrosion Protection for the Deployment Environment
Compare Aluminum, Coated Steel, and Stainless Steel by Application
Material selection should consider stiffness, weight, fabrication, welding, electrical continuity, corrosion exposure, coating compatibility, and lifecycle cost. Coated steel may suit many moderate environments; aluminum can reduce weight; stainless steel may suit more demanding exposure but can increase material and fabrication cost. No single option fits every outdoor telecom cabinet.
Substitutions should require approval because alloy, coating, or temper changes may affect bending, welding, grounding, and corrosion.
CK Metal Tech’s precision sheet metal manufacturing capabilities include laser cutting, punching, bending, riveting, welding, and processing of stainless steel, carbon steel, aluminum alloy, galvanized sheet, and aluminum-zinc-coated sheet. Suitability still depends on the drawing and deployment requirements.
Prevent Edge, Fastener, Weld, and Galvanic Corrosion
Corrosion commonly starts at cut edges, holes, welds, scratches, fasteners, and uncoated grounding areas. These locations may have thinner protection, heat-affected surfaces, trapped moisture, or dissimilar-metal contact.
The RFQ should identify substrate, pretreatment, coating system, masking, fastener material, repair method, and acceptance criteria. Where different metals meet, review galvanic compatibility and consider isolation or sealing.
A salt-spray duration alone is incomplete. Buyers should also define specimen condition, scribe method if applicable, evaluation criteria, and how the laboratory test relates to actual service exposure.
Validate the Prototype Before Repeat Production
Define Test Ownership and the Required Assembly State
Thermal, EMC, ingress, corrosion, and mechanical checks may involve different parties. Thermal and EMC acceptance may require actual electronics, cables, software load, and cooling components.
Testing an empty enclosure may not represent the completed system. Cable glands, vents, locks, mounting plates, and purchased hardware can change sealing, airflow, and electrical continuity. Define the test sample, assembly state, test owner, report format, and approval authority. Before repeat production, freeze approved drawings, materials, gaskets, masking, and inspection points.
Review Common Failure Modes Before Production Approval
| Failure mode | Likely issue | Next action |
|---|---|---|
| Internal overheating | Heat input or cooling path undefined | Recheck heat load and assembled airflow |
| Condensation | Temperature cycling or moisture path overlooked | Review venting, drainage, heating, and shutdown conditions |
| EMC leakage | Continuity lost at a seam or penetration | Inspect bonding paths and retest the system |
| Water ingress | Gasket compression or cable entry inconsistent | Test the final assembled enclosure |
| Edge corrosion | Edges, welds, or fasteners lack protection | Review pretreatment and local repair |
| Door misalignment | Fabrication or coating changed geometry | Correct datums and assembly controls |
Prepare a Comparable RFQ and Qualify the Manufacturer
Include the Technical Inputs Required for a Quote
A custom telecom enclosure RFQ should include controlled 2D drawings, a 3D model, BOM, equipment layout, weight, heat dissipation, installation site, mounting method, ambient conditions, ingress requirements, EMC interfaces, material, finish, grounding points, cable entries, prototype quantity, annual volume, testing, assembly, and packaging.
When requirements remain open, request a DFM review and prototype quotation rather than a production price based on assumptions. The quotation should identify drawing revision, included components, outsourced processes, testing responsibility, and exclusions.
Evaluate Supplier Capabilities, Evidence, and Red Flags
A qualified manufacturer should explain the route from cutting and bending through joining, finishing, inspection, assembly, and packaging. Ask how door alignment, gasket compression, conductive contact areas, masked features, cable openings, and engineering changes are controlled. Warning signs include unsupported “6G-ready,” “IP-rated,” or “EMC-shielded” claims, quotations without revision references, and no distinction between enclosure inspection and complete-system validation.
CK Metal Tech provides precision metal manufacturing and assembly capabilities covering sheet metal processing, machining, stamping, surface finishing, and component assembly. Its website also lists communication enclosure products; the suitable process remains dependent on material, geometry, quantity, and application.
Conclusion
A telecom enclosure for future 6G equipment should be specified through measurable project conditions, not a future-ready label. Define the equipment, environment, heat load, EMC interfaces, moisture risks, corrosion exposure, maintenance access, and verification responsibility before comparing suppliers.
Buyers can submit telecom enclosure drawings for a manufacturing review with the model, dimensions, material, site conditions, heat information, quantity, finish, testing expectations, and assembly scope. CK Metal Tech can then review the manufacturing route without treating unconfirmed thermal, EMC, ingress, or corrosion performance as an established product claim.
Frequently Asked Questions
Is there a final 6G telecom enclosure standard?
No universal final standard defines the material, cooling route, IP rating, or corrosion class for every 6G enclosure. Requirements should come from the specific equipment, deployment environment, applicable standards, and customer test plan.
How do you cool a sealed telecom enclosure?
The suitable method depends on internal heat, ambient temperature, solar exposure, enclosure size, allowable temperature, and ingress requirements. Options may include passive dissipation, heat exchangers, or sealed active cooling, subject to engineering verification.
How does powder coating affect EMC shielding?
Powder coating is electrically insulating and may interrupt grounding or bonding at doors, panels, fasteners, and contact surfaces. Drawings should identify masked conductive areas and final EMC test requirements.
Which material is suitable for an outdoor telecom cabinet?
The choice depends on weight, stiffness, fabrication, corrosion environment, coating system, electrical bonding, maintenance, and lifecycle cost. Material grade and finish should be verified against the deployment specification.
What information is needed for a custom telecom enclosure quote?
Provide drawings, BOM, equipment arrangement, weight, heat dissipation, installation method, environment, ingress and EMC requirements, material, finish, quantity, testing, assembly, and packaging.